China has become a major manufacturing base for packaging machinery, including the Chipboard Slotting Machine. Its supplier landscape combines large factories, specialized engineering teams, and export-focused service networks. Yet, “top supplier” should never mean the lowest quoted price. It should mean proven accuracy, stable production, documented testing, and dependable support after delivery.
Industry data supports this growing demand. Smithers’ report, The Future of Corrugated Packaging to 2028, identifies continued expansion in corrugated packaging production, driven by e-commerce, food delivery, and retail logistics. The report also highlights pressure for faster converting and improved material efficiency. These trends directly influence slotting equipment requirements. A reliable machine should create clean slots, maintain consistent dimensions, and handle repeated production without excessive downtime.
Small details matter.
For example, operators should inspect slot depth, blade alignment, feeding stability, and dust control during factory demonstrations. A strong Chinese supplier should provide technical drawings, sample testing, electrical specifications, spare-parts guidance, and clear installation procedures. ISO 9001 certification can support process credibility, but certification alone does not prove machine performance. Independent testing and customer references remain valuable.
This guide examines how to identify China’s leading Chipboard Slotting Machine supplier. It considers machine structure, automation, customization, safety design, delivery capability, and after-sales service. However, no supplier is perfect. Buyers should question optimistic claims and compare measurable results. A careful evaluation may take longer, but it can prevent costly production interruptions later.
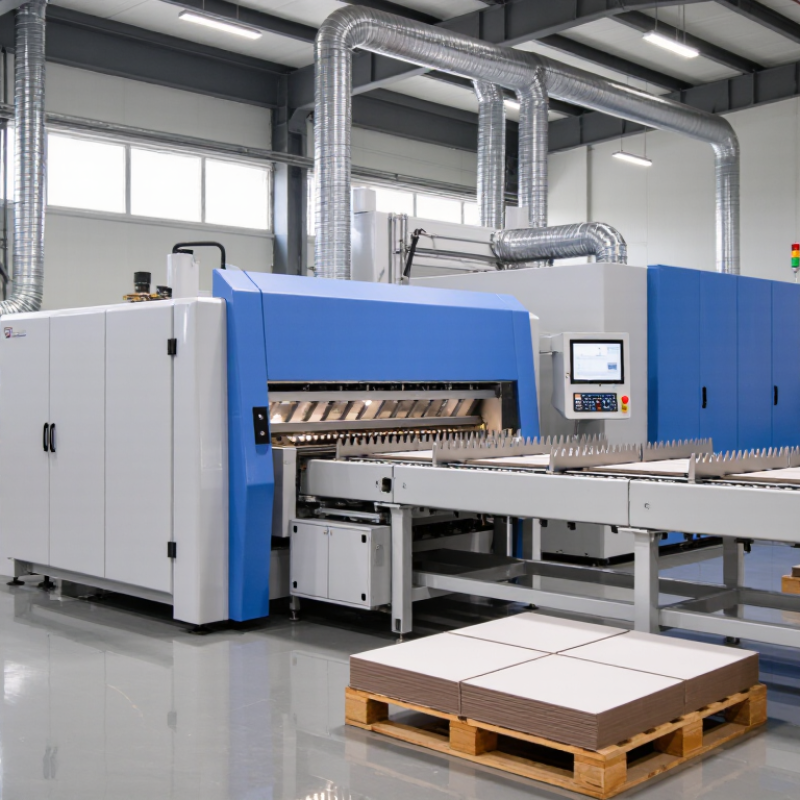
A chipboard slotting machine is industrial equipment designed to cut precise grooves in chipboard panels. These grooves can hold shelves, dividers, back panels, or connecting components. The machine uses rotating blades, guide rails, and adjustable stops to control cutting depth and position. Some models process one panel at a time, while automated systems handle continuous production. Clean slots matter. Rough edges can weaken joints and increase assembly problems.
In practical production, operators place a panel on the working table and set the required slot size. The blade then removes a narrow strip of material with controlled movement. Dust extraction is important because loose particles can affect visibility and cutting accuracy. From hands-on observation, blade sharpness often changes the final result more than expected. A dull blade may create chipped edges, even when the settings appear correct. My early assumption was different. Machine accuracy alone does not guarantee a perfect panel.
Tips: Measure the first slot carefully. Check blade wear before each shift. Keep the table clean and level. Test a spare panel before full production. Small errors multiply quickly. Operators should also inspect slot depth with a simple gauge, rather than relying only on machine displays. Moisture, panel density, and surface coating can change cutting behavior. A stable process still needs regular adjustment.
A practical overview of chipboard slotting machine functions, configurations, operating data, and production considerations.
| Data Dimension | Typical Information | Practical Relevance | Key Consideration |
|---|---|---|---|
| Machine Definition | A woodworking machine designed to cut straight grooves, slots, channels, or rebates in chipboard and similar panel materials. | Supports furniture assembly, cabinet construction, shelving, drawer components, and panel-joining applications. | The machine should be selected according to panel thickness, slot dimensions, production volume, and required accuracy. |
| Common Workpiece Materials | Plain chipboard, melamine-faced chipboard, laminated particleboard, MDF, plywood, and some composite panels. | Different materials can be processed with suitable cutters, cutting speeds, clamping methods, and dust extraction. | Melamine and laminated surfaces require sharp, suitable tooling to reduce chipping and edge damage. |
| Main Slotting Operations | Longitudinal slots, cross slots, T-slots, back-panel grooves, dadoes, edge grooves, and shallow rebates. | These operations allow panels to interlock or receive shelves, backs, dividers, fittings, and hardware. | The cutter profile and machine travel must match the required slot geometry. |
| Typical Panel Thickness | Approximately 6–40 mm for many woodworking applications; the actual range depends on machine design. | Covers common furniture panels, shelving boards, cabinet sides, and back-panel materials. | Confirm the maximum workpiece thickness and the available vertical or horizontal adjustment before purchase. |
| Typical Slot Width | Common production requirements are approximately 3–12 mm, although wider or custom slots are possible with appropriate tooling. | Slot width determines the fit of shelves, joining components, spline materials, and back panels. | The cutter diameter, kerf, and material compression must be considered to achieve the intended fit. |
| Typical Slot Depth | Often approximately 2–15 mm for furniture-related grooves, subject to panel thickness and structural requirements. | Controls joint engagement and helps prevent cutting through the panel. | The depth should be adjusted to preserve sufficient remaining panel thickness and surface integrity. |
| Machine Configuration | Available formats include manual, semi-automatic, automatic, vertical, horizontal, single-spindle, multi-spindle, and CNC-controlled systems. | Configuration affects setup time, repeatability, labor requirements, and production capacity. | CNC systems are useful for variable patterns, while dedicated machines can be efficient for repetitive slotting. |
| Spindle Speed | High-speed woodworking spindles commonly operate within roughly 12,000–24,000 revolutions per minute, depending on the cutter and machine. | Suitable speed helps balance cutting quality, tool life, noise, heat generation, and productivity. | Always follow the cutter manufacturer’s maximum speed and recommended cutting parameters. |
| Feed Rate | A broad woodworking range is approximately 3–20 m/min, depending on material, cutter diameter, spindle power, and surface requirements. | Feed rate influences throughput, edge quality, cutting force, and the risk of burning or chipping. | Use lower starting values for laminated surfaces or unfamiliar materials, then optimize through testing. |
| Positioning Accuracy | CNC machines may commonly target approximately ±0.05–0.20 mm positioning accuracy; actual cutting accuracy depends on the complete system. | Accurate positioning improves joint consistency and interchangeability between panels. | Machine rigidity, calibration, tooling condition, panel tolerances, and environmental factors also affect results. |
| Workholding Method | Common methods include mechanical clamps, pressure beams, stops, fixtures, and vacuum tables. | Stable workholding reduces vibration, movement, dimensional errors, and surface damage. | Vacuum or automated clamping is useful for repeat production, while mechanical fixtures may suit smaller batches. |
| Cutting Tools | Carbide-tipped straight cutters, slotting saws, compression cutters, and specialized profile tools are commonly used. | Tool selection affects slot dimensions, edge finish, service life, and resistance to chipping. | Choose a tool suitable for abrasive particleboard and the presence of decorative laminates. |
| Dust Extraction | A dedicated dust-collection system is normally required because chipboard machining produces fine wood and resin particles. | Effective extraction improves visibility, surface quality, equipment cleanliness, and workplace air quality. | Extraction capacity, hose diameter, filter maintenance, and enclosure design should be checked as a complete system. |
| Production Suitability | Manual machines suit low-volume or flexible work; automatic and CNC machines suit repeatable medium- and high-volume production. | The correct automation level can reduce setup time, operator workload, and material handling effort. | Evaluate cycle time, changeover frequency, operator skill, floor space, and integration with other equipment. |
| Safety Requirements | Important features include guarding, emergency stops, interlocks, secure clamping, dust control, and safe tool-changing procedures. | Proper safeguards help reduce risks from rotating tools, ejected particles, noise, dust, and unexpected machine movement. | Operators should receive training and follow applicable workplace safety regulations and maintenance procedures. |
How Does a Chipboard Slotting Machine Work?
A chipboard slotting machine converts flat sheets into accurate folding panels. The operator places chipboard on the feeding table. Rollers then move each sheet toward adjustable guides. A rotating scoring wheel compresses fold lines without cutting through the board. The slotting unit removes narrow sections from selected edges. These openings help panels fold cleanly and form rigid boxes. Sensors monitor sheet position, while a collection system removes scraps. Small errors matter. Misaligned slots can create uneven corners or weak folds.
According to Mordor Intelligence, the global paper packaging market was valued at about US$427 billion in 2024. It may reach approximately US$540 billion by 2029. This growth increases demand for faster and more consistent converting equipment. Yet speed alone is not enough. Board moisture, thickness, and grain direction affect slot quality. A machine may perform well during testing, but production dust can change results. Regular inspection remains essential.
Tips: Check blade clearance before each shift. Use a sample sheet to confirm slot depth and spacing. Keep feeding rollers clean. Measure the first ten pieces, not only the first one. If folding feels unusually stiff, reduce pressure and inspect the scoring line. Operators sometimes trust digital settings too much. Physical samples still reveal problems that screens miss.
China-made chipboard slotting machines are built for accurate grooves, repeatable production, and practical workshop use. A rigid steel frame helps reduce vibration during cutting. This matters when panels are large or slightly uneven. Servo-driven positioning can improve slot accuracy and reduce manual adjustment. However, performance depends on calibration, tooling, and operator training.
A useful machine should support adjustable slot width, depth, and spacing. Digital controls make these settings easier to record and repeat. Some models include automatic feeding, dust collection ports, and emergency stop systems. These features improve workflow and workplace safety. They also reduce unnecessary handling around the cutting area. In production trials, clean chip removal often affects accuracy more than expected. Dust can hide the cutting line and shorten tool life.
Reliable suppliers should provide clear technical drawings, load data, spare-part information, and operator instructions. They should also explain tolerance limits instead of promising perfect results. This point deserves attention. No slotting machine performs equally well with every chipboard grade. Board density, moisture, and surface coating can change the cutting response. Buyers should request sample testing before placing a large order. A machine may look impressive in a showroom, yet require careful setup on the factory floor. Practical support, honest specifications, and accessible maintenance guidance are key features worth checking.
China Top Chipboard Slotting Machine Supplier? How to Choose a Reliable Chinese Supplier
Choosing a Chinese chipboard slotting machine supplier requires more than comparing quotations. Fortune Business Insights valued the global corrugated packaging market at about USD 205.44 billion in 2023. It forecasts approximately USD 270.83 billion by 2032. This growth increases demand for stable, accurate converting equipment. Ask for measurable results, not attractive promises. Request cutting accuracy, slot-depth tolerance, production speed, and motor-load data for your board grade. A serious supplier should provide test videos using your actual chipboard. Paper samples are not enough.
Inspect the factory’s quality process. Check incoming material records, assembly inspections, electrical testing, and final trial reports. ISO 9001 certification can support consistency, but it does not guarantee machine performance. Verify the certificate independently. Ask how quickly spare parts are supplied and whether manuals include wiring diagrams, lubrication points, and fault codes. Remote commissioning is useful. Local technical support is better. I would not trust a polished factory tour alone. A supplier may pass an audit and still miss your required slot depth. Include acceptance standards in the contract, including sample approval, noise limits, training, packaging protection, and response times. Review at least three years of export references, while remembering that references can be selective. A live video call with an operating machine is more convincing than a brochure.
This illustrative supplier-evaluation model assigns the highest weight to technical fit and build quality because slotting accuracy, machine stability, and compatibility with the buyer’s production requirements directly affect long-term performance. Buyers should verify each score through samples, factory audits, references, warranty terms, and documented delivery records.
Global demand makes consistency important. FAO’s 2022 Forestry Production and Trade data recorded more than 390 million cubic metres of wood-based panels worldwide. Chipboard slotting machines must handle changing densities, recycled content, and surface finishes without damaging edges.
A capable supplier should document inspections under ISO 9001 procedures. Ask for spindle runout results, cutting-depth tolerance, electrical test records, and factory acceptance data.
ISO 12100 supports machine risk assessment, while IEC 60204-1 addresses electrical safety.
For panels, EN 312 requirements help define particleboard performance, although local specifications may differ.
A practical test should use your actual board thickness and groove design. Samples can reveal burning, tear-out, or loose dust that a catalogue hides.
Applications include cabinet backs, furniture joints, shelving, flooring components, and lightweight interior partitions.
Maintenance begins with dust extraction. Fine particles can enter bearings, sensors, and control cabinets. Operators should inspect cutters each shift, check clamping pressure, and verify groove depth with a calibrated gauge.
Lubrication intervals should follow the machine manual, not guesswork. In my experience, rushed cleaning causes more downtime than ordinary cutting wear. That assumption deserves review. Record vibration, motor temperature, tool changes, and rejected pieces; small trends often appear before visible failure.
1272 Speers Rd Unit 4
Oakville ON Canada L6L 2X4
©Copyright 2020 Gosco Valves. All rights reserved.