Why Do Manufacturers Use Weld Fixture Tooling?
Manufacturers use Weld Fixture Tooling to hold parts in the right position while welds are made. A fixture can locate panels, brackets, or frames against repeatable reference points. Clamps then help limit movement during tacking and welding. The result is a more consistent assembly, not a guarantee of a perfect one.
Small details matter. A few millimeters of misalignment can affect fit-up, gaps, and downstream assembly. Well-planned tooling can reduce repeated measuring and manual repositioning, while giving operators clearer access to the joint. Designers also consider clamp locations, loading sequence, weld access, and part removal. Heat can still distort metal, so a fixture must support the work without blocking the weld or creating unnecessary stress. Its effectiveness depends on the part, process, and operator.
The value is practical: fewer avoidable variations, smoother handling, and a more repeatable production routine. But more tooling is not always better. A complex fixture may cost more, take longer to adjust, or become a problem when product designs change. Manufacturers therefore weigh production volume, tolerances, material behavior, and maintenance needs before choosing a setup. That judgment can be imperfect. Real parts and shop conditions do not always match the drawing. Understanding why manufacturers use Weld Fixture Tooling means looking beyond clamps and steel: the goal is controlled positioning that supports quality, safety, and efficient work without promising that tooling alone can solve every welding challenge.
What Weld Fixture Tooling Is and How It Works
Why Do Manufacturers Use Weld Fixture Tooling?
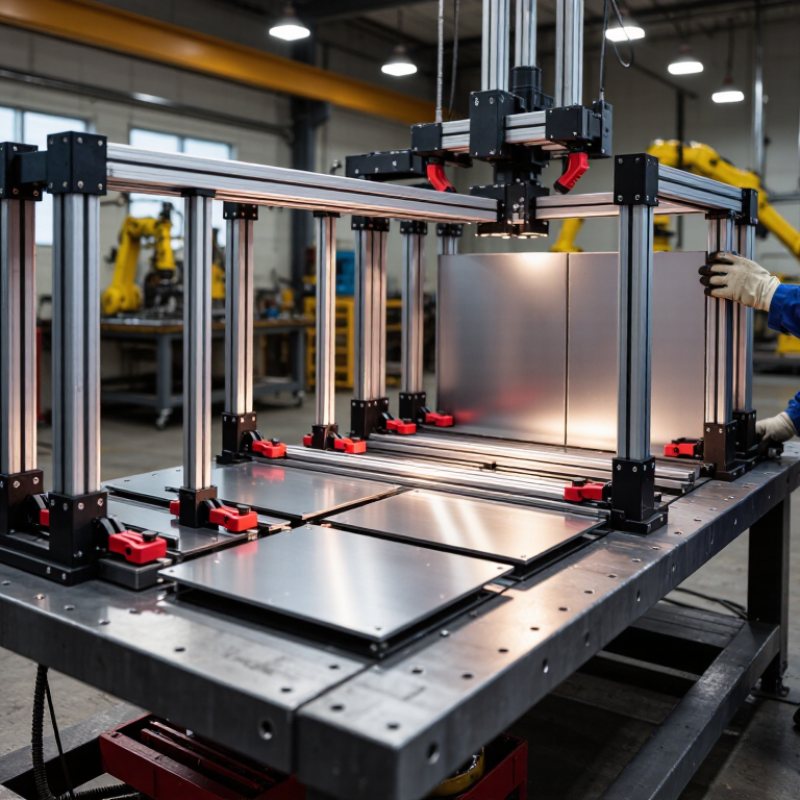
Weld fixture tooling holds parts in a controlled position while they are joined. A typical fixture uses a sturdy base, locating pins, stops, and clamps. These components guide each workpiece to the intended location and help maintain joint alignment. Small details matter. A few millimeters of movement can affect fit, weld quality, or later assembly.
In use, an operator places the parts against the fixture’s locating points and secures them with clamps. The weld is then made while the fixture resists movement from handling and heat. Some setups are manual; others use pneumatic or hydraulic clamping. The design must leave enough room for the torch, the operator’s hands, and inspection. It also needs to account for heat expansion. A fixture that clamps too rigidly can sometimes contribute to distortion rather than prevent it.
Manufacturers check a fixture with trial welds and measurements before relying on it for repeat production. They may adjust stops or clamping pressure when parts vary slightly. That part is easy to underestimate. Fixtures also wear, collect spatter, and need regular cleaning and checks. They improve consistency, but they cannot correct poor joint preparation or an unsuitable welding sequence.
Why Manufacturers Use Weld Fixture Tooling
A weld fixture locates and holds parts in position during welding, helping maintain alignment and repeatability. This chart illustrates the classic 3-2-1 locating principle: three contacts on the primary plane, two on the secondary plane, and one on the tertiary plane. Clamps hold the parts against the locators; actual fixture designs vary by part and process.
Why Welded Parts Need Accurate Positioning and Restraint
A welded assembly can move before the final bead cools. Heat expands the joint, then contraction can pull a bracket out of square or lift a thin panel from its locating surface. Accurate positioning gives each component a repeatable starting point; restraint limits movement while the weld sequence adds heat. Small shifts matter. A hole that misses its mating pin by a few millimetres can complicate downstream assembly.
ISO 13920:1996 provides general tolerance classes for welded constructions. Its Class B table allows ±2 mm for linear dimensions from 2 to 30 mm, showing how tightly even short features may be controlled. A fixture should therefore locate from stable datums, support flexible sections, and clamp near the joint without blocking torch access. Too much restraint can create its own problems, including stress concentration and difficult unloading. That trade-off deserves a real trial. Check the part after release, not only while it remains clamped; springback can reveal a gap between fixture accuracy and finished-part accuracy. Weld sequence, clamp position, and part thickness all affect the result, so a fixture that works for one assembly may need adjustment for another.
How Fixtures Improve Weld Quality and Repeatability
Why Do Manufacturers Use Weld Fixture Tooling?
How Fixtures Improve Weld Quality and Repeatability
A weld fixture holds parts in a defined position while they are joined. Clamps and locating pins help control gaps, angles, and alignment. This matters when a joint must meet the same dimensions across many assemblies. For example, a fixture can keep two steel brackets square while heat pulls at the seam. Stable positioning also helps welders maintain a consistent torch path and reduces time spent correcting misplaced parts. Small shifts matter.
Tips: Check locating points for wear, and remove spatter before it changes how a part sits. Confirm that clamps hold securely without distorting thin material. A simple fit check at the start of a shift can catch problems early.
Fixtures support repeatability, but they are not a cure-all. Poor fit-up, inconsistent heat input, or worn components can still produce defects. A fixture may also restrict access to a joint, so its design should suit the weld sequence and inspection needs. Teams should review actual parts, not rely only on drawings; real components can vary slightly. Recording setup checks and maintenance findings helps operators spot gradual changes before they affect a batch. The process takes attention, and that can be easy to underestimate.
How Weld Fixtures Increase Production Efficiency and Safety
Why Do Manufacturers Use Weld Fixture Tooling?
Weld fixtures help operators locate parts in the same position for each weld. Pins, stops, and clamps keep components steady while the joint is formed. This reduces repeated measuring and makes it easier to maintain consistent fit-up across a production run. Small gains matter.
A stable fixture can also improve safety at the work cell. It limits part movement and reduces the need to hold pieces by hand near the welding area. Thoughtful access points let operators clamp and release parts without awkward reaching. Fixtures do not replace training, protective equipment, or safe welding procedures, but they can support better work habits.
Efficiency depends on the details. A fixture that loads quickly and leaves room for the torch can shorten cycle times and reduce rework. Clear locating features also help new operators understand where each component belongs. Yet a complicated fixture may slow changeovers or make cleaning difficult. That trade-off is easy to overlook. Reviewing operator feedback and checking worn clamps or locating pins helps keep the tooling useful, not just precise on paper.
Where Weld Fixture Tooling Is Used in Manufacturing
Why Do Manufacturers Use Weld Fixture Tooling?
Where Weld Fixture Tooling Is Used in Manufacturing
Weld fixture tooling appears wherever parts must stay aligned during welding. In automotive plants, fixtures hold body panels, doors, and chassis members at repeatable positions. A clamp or locating pin can prevent heat from pulling a joint out of alignment. Similar tooling supports frames for agricultural machinery, appliances, railcars, and construction equipment. The designs vary. The need for stable parts does not.
The International Federation of Robotics’ World Robotics 2024 report counted 4.28 million industrial robots operating worldwide in 2023, a 10% increase from 2022. That figure reflects growing automation, not fixture use directly. Still, automated welding cells depend on accurately located workpieces. Fixtures also serve manual welding stations, where operators need clear access and consistent joint gaps. In practice, a fixture that is too complex can slow changeovers or obstruct a weld.
Tips: Check clamp access, heat distortion, and part variation before finalizing a fixture. Fit matters. Test it with real components, not only drawings. A small mismatch can become a repeated defect, and even experienced teams sometimes overlook it.


